- This topic is empty.
-
AuthorPosts
-
2026-10-29 at 3:54 pm #11022
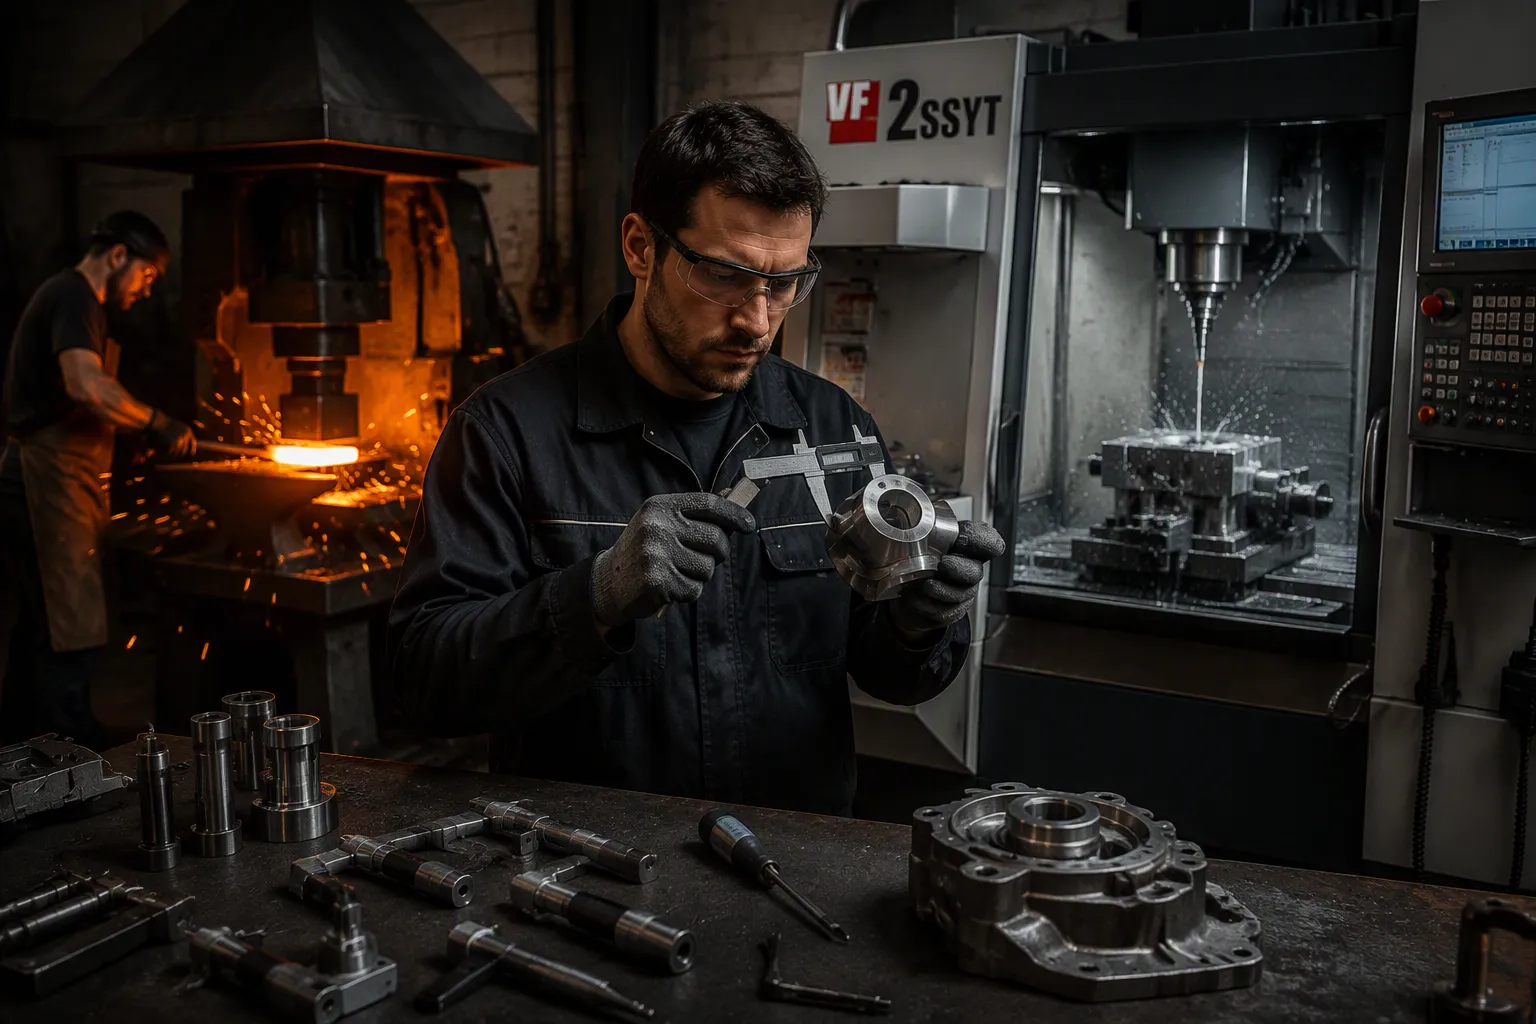
Image Source: https://www.xuxiangtaimetal.com Forging and precision machining are complementary processes. Forging builds strength and continuous grain flow into the part. Machining delivers the exact dimensions and features the design requires. Together they produce custom mechanical parts that are both strong and accurate. Neither process achieves this result as efficiently alone. This combination is standard practice for load-bearing industrial components. Performance and fit both matter in these applications. This article is written as a professional English B2B educational article for US mechanical engineers. It explains how the two processes work as partners.
Key Takeaways
- Forging builds strength into parts by aligning grain flow, while precision machining delivers exact dimensions and features.
- An integrated workflow reduces costs, lead times, and errors by combining forging and machining under one quality system.
- Choose forging plus machining for high-volume, load-bearing parts; choose machining from solid for low-volume or complex prototypes.
Forging Builds Strength Into the Part
What Forging Does
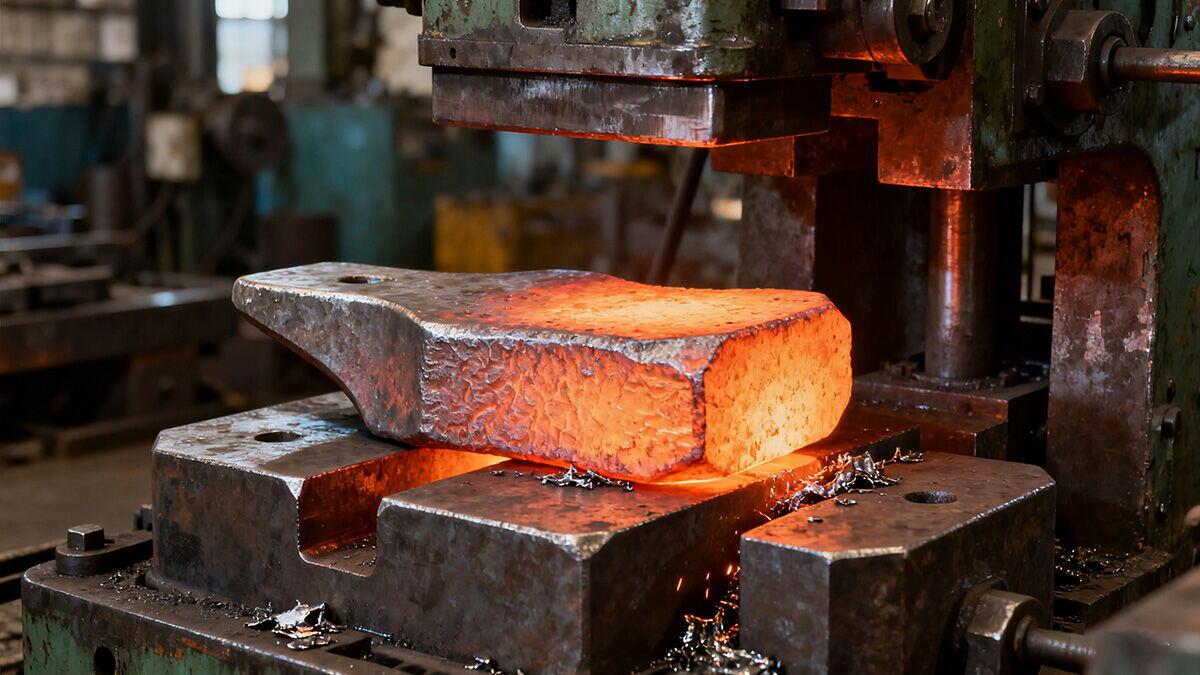
The forging process shapes metal through controlled deformation at elevated temperatures. A press or hammer applies force to a heated billet, and the metal flows into the die cavity. This action produces a dense, cohesive structure. Forging removes internal voids left after solidification. The result is a forged metal component with predictable, uniform mechanical properties.
Grain Flow and Mechanical Advantages
Grain flow orientation governs how a part performs under stress. Forging aligns grains along the primary stress paths of the component. This alignment delivers several measurable benefits:
- Increased strength and fatigue resistance, which is critical in rotating parts such as shafts and gear blanks.
- Enhanced impact toughness, so the material absorbs energy under sudden loads.
- Improved structural integrity through the elimination of internal voids and discontinuities.
- Directional performance optimization, where grain flow matches the load-bearing surfaces of the part.
Machining from rolled bar interrupts this natural grain structure. The forging process preserves and enhances grain continuity instead. A forged shaft keeps grain flow along its longitudinal axis for maximum torsional strength. A seamless rolled ring develops circumferential grain flow for rotational stability.
Common Forged Parts
Load-bearing custom mechanical parts appear across many industries. The table below shows representative examples.
Industry Representative forged load-bearing parts Automotive Crankshafts, gears, connecting rods, axles Oil and gas Flanges, valves, fittings, pressure components Power generation Turbine shafts, generator components, structural components Heavy engineering and construction Crane and excavator parts for heavy loads and extreme conditions Mining and heavy machinery Shafts, gears, rings, structural components These applications share one requirement: reliable performance under repeated or impact loads. Forging meets that requirement through controlled grain flow and a dense material structure.
Precision Machining Delivers Accuracy
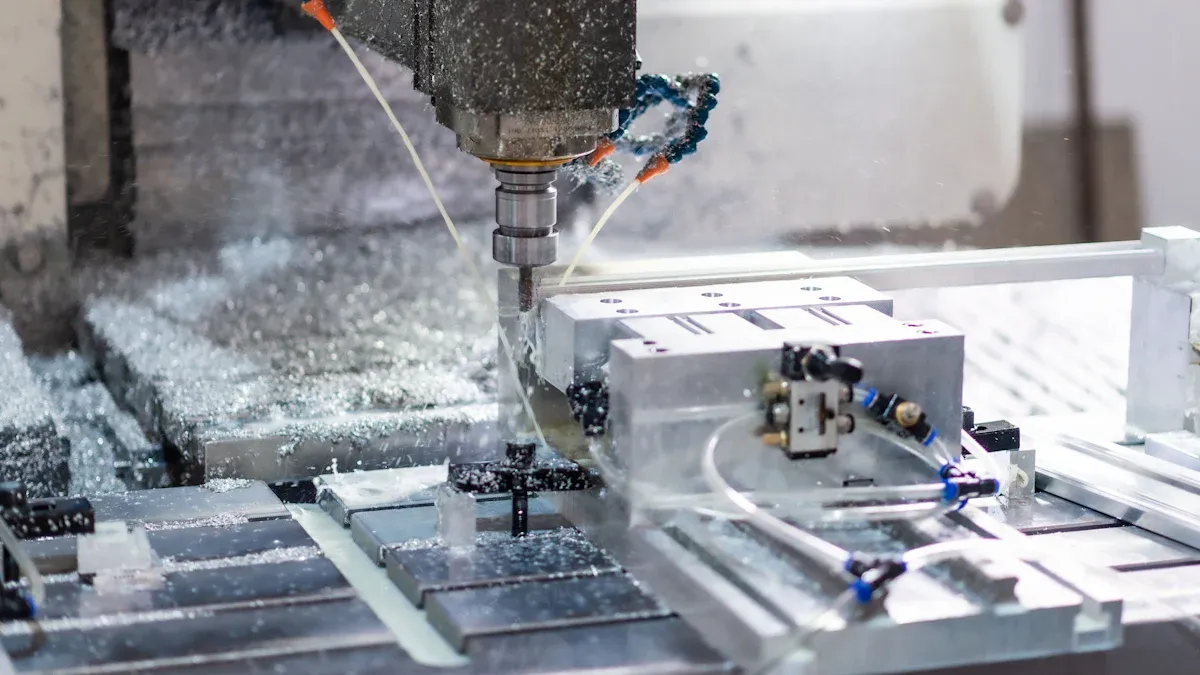
Image Source: https://www.xuxiangtaimetal.com The Role of CNC Machining
Precision machining removes material from a forged blank to create the final geometry. CNC equipment controls the cutter path through programmed coordinates. This control produces repeatable results across every part in a production run. Common operations include turning, milling, drilling, boring, and grinding. Each operation suits a different feature type. Turning creates cylindrical surfaces such as shafts and bearing bores. Milling forms flats, slots, and pockets. Grinding refines surfaces to a very smooth condition. The forging process establishes the rough shape, and CNC work brings that shape to final size.
Tolerances and Critical Features
Tolerance capability defines what precision machining can deliver. Most shops apply standard tolerance blocks of ±0.005 in (±0.127 mm) for general dimensions. Tight features such as bearing bores and locating pins hold ±0.002 in (±0.050 mm). Precision surfaces reach ±0.001 in (±0.025 mm). Turned shaft diameters on a lathe can hold ±0.00016 in (±0.004 mm).
Critical features on forged metal components typically include:
- Datums and GD&T that define relationships between features
- Concentricity or runout on rotating features
- Thread specifications, including size, pitch, and tolerance class
- Mating diameters and surfaces that control fit and assembly
- Surface roughness on functional surfaces
- Critical hole locations and assembly dimensions
Each tolerance should tie to a functional need such as fit, alignment, sealing, or rotation. Not every dimension deserves equal criticality.
When Machining Leads
Some custom mechanical parts are machined from solid stock instead of forged blanks. This choice fits certain scenarios well.
Scenario Why machining from solid fits Tight tolerances required As-forged surfaces are dimensionally loose; CNC holds ±0.005 in or tighter Complex geometry or intricate features Tight-tolerance bores and thin-wall sections belong to CNC work Small batches or prototypes Low volume does not justify forging tooling Tooling investment not justified by volume Forging setup costs pay off at higher volumes Static-load precision components Machined-from-billet parts perform well where cyclic fatigue is not the driving load case For OEM manufacturing programs with high volume and load-bearing duty, forging plus machining remains the stronger path. For low volume or intricate geometry, machining from solid offers a practical alternative.
How Forging and Precision Machining Work Together for Custom Mechanical Parts
The Typical Production Sequence
An integrated workflow follows a defined order. Each stage prepares the part for the next one. This guide is written as a professional English B2B educational article for US mechanical engineers, and the sequence below reflects standard shop practice.
- Raw material selection. The shop verifies the steel grade, heat number, and mill certification before cutting any billet.
- Precision forging. A press or hammer forms the heated billet into a near-net shape. The die cavity controls the rough geometry and the grain flow direction.
- Heat treatment. Normalizing, quenching, and tempering establish the required hardness and microstructure.
- CNC machining. Turning, milling, drilling and tapping, broaching, grinding, and precision finishing bring the part to final geometry.
- Gear manufacturing. Hobbing, shaping, gear grinding, a second heat treatment, and inspection apply to toothed components.
- Surface finishing. Coating, plating, or shot peening protects the part and conditions its surface.
- Quality inspection. Dimensional, metallurgical, and non-destructive checks confirm compliance with the drawing.
- Packaging and dispatch. Protected parts move to assembly or to the customer.
The machining stage deserves closer attention. CNC turning, CNC milling, drilling and tapping, broaching, grinding, and precision finishing each address a different feature class. These operations achieve tight tolerances on diameters, threads, bearing seats, holes, and keyways. Machining after an optimized forging reduces material removal and waste.
The forging stage leaves stock on the part by design. Two terms describe this stock:
- Finish allowance, also called machining allowance or forging envelope, is the quantity of stock retained on the forging surface for removal during later machining.
- Finish all over (F.A.O.) is a specification that requires the forging to be oversized relative to the drawing dimensions so every surface can be machined. The extra stock is not a fixed figure. It varies with part size and shape and is mutually agreed upon by the vendor and the user.
A well-planned allowance balances two goals. Too much stock wastes material and machining time. Too little stock risks incomplete cleanup on a critical surface.
Benefits of the Integrated Approach
The integrated model delivers measurable gains in cost, lead time, and quality. Near-net forged components require less machining. This reduces material waste, machining time, and overall production costs while improving manufacturing efficiency. Internal coordination between departments also reduces transportation delays and eliminates unnecessary waiting between manufacturing stages. Shorter lead times follow.
Cost-Saving Benefit How It Reduces Cost Reduced material waste Near-net-shape forging minimizes material removed during machining Lower machining time Less machining needed, enabling faster cycles and lower costs Lower overall production expenses Using lower-cost manufacturing regions for initial forging Material and time savings Near-net-shape forgings minimize scrap and shorten production cycles Supply chain structure matters as much as shop-floor efficiency. One integrated supplier describes the hidden cost of split sourcing this way:
“In a traditional supply chain, ‘transit dead time’ can account for up to 30% of the total production schedule… We reduce internal supply chain expenses and freight costs by condensing management processes and reducing the number of purchase orders.”
Quality improves alongside cost. A single unified quality assurance protocol covers metal shaping, thermal processing, and finish machining. This structure removes the logistical delays and dimensional hand-off errors that occur when separate vendors handle forging and machining. Hand-off errors between separate vendors are a key contributor to part rejection. Eliminating them directly lowers rejection rates. Integrated suppliers report that customers choose this model specifically to solve high rejection rates, dimensional inconsistencies, fatigue failures, unstable supply chain quality, and inconsistent machining from local vendors. Separate forging and machining arrangements cannot address these problems as effectively.
Forging vs. Machining: Strength, Precision, and Cost
The two processes are partners, not competitors. Each one leads in a different performance dimension. A professional English B2B educational article for US mechanical engineers should make this distinction clear, because the choice drives design decisions.
Strength favors the forging process. Forged parts carry grain flow aligned with the part shape. Machining cuts through that flow. The mechanical differences are substantial.
Property Forged Parts Machined Parts Tensile Strength ~26% higher than cast/machined Baseline (lower) Fatigue Strength ~37% higher than cast/machined Baseline (lower) Fatigue Life Long Shorter Grain Flow Aligned with part shape Cut through by machining Internal Defects Eliminated or minimized Remain from original material Documented test results reinforce the gap. One comparison raised tensile strength 50%, from 500 MPa on a machined shaft to 750 MPa on a forged shaft. The fatigue limit rose from 200 MPa to 300 MPa, also a 50% gain. The forged shaft survived 1,000,000 cycles at 100 Nm torque. The machined version fractured before 1,000 cycles. Cold-rolled threads, a cold forging process, delivered four times the fatigue lifetime of machined threads. Residual compressive stresses at the thread roots and an aligned grain structure slow crack initiation and propagation.
Precision favors precision machining. CNC work offers extremely high precision and flexibility, especially for complex-shaped components, with stable and highly repeatable production. It achieves dimensional accuracy and complex geometry that forging cannot form directly, including micro-features, curved surfaces, and precise hole positions. Forging suits parts with relatively simple shapes and high strength requirements. Complex geometries usually need additional machining after forging for finishing and correction.
Comparison Aspect Precision Forging CNC Machining Dimensional Accuracy Higher than conventional forging; tolerances of ±0.3 mm to ±1.0 mm Extremely high precision; tighter dimensional tolerances than forging Machining Allowance Reduced but not eliminated Used to achieve final tolerances and surface finishes Best Use Case Simple shapes with high strength and dimensional consistency High-precision, complex geometries and tight tolerances The division of labor is straightforward. Forged parts deliver superior grain alignment and high fatigue strength, which makes them ideal for load-bearing applications. Machined parts achieve tighter dimensional tolerances and smoother surfaces through precision cutting. Precision forging improves dimensional stability and repeatability compared with conventional forging. It does not eliminate machining. CNC work is still required to reach final tolerances, surface finishes, or functional features. Combining both processes balances forming efficiency with final dimensional accuracy.
Cost follows production volume. Forging carries higher initial tooling cost and lower unit cost in bulk. Machining carries lower setup cost and higher per-unit cost. Machining also tends to be more expensive than forging because it removes material rather than forming it. Longer processing times and higher labor and machine costs follow, particularly for complex parts.
Production Scale Forging Machining High-volume Higher initial tooling/setup cost, but unit cost drops as volume rises; high material utilization lowers overall cost Longer processing times and greater material waste raise per-unit cost at scale Low-volume / custom Less economical due to tooling investment No expensive tooling needed, quick adjustments, suitable for small batches For OEM manufacturing programs with high volume and load-bearing duty, forging plus machining is the stronger economic path. For prototypes and small batches, machining from solid avoids tooling investment. Many programs use both routes across a product family.
Quality Control at Each Stage
Quality control in an integrated workflow is continuous, not a final gate. Each stage has its own checkpoints, and the data carries forward.
Forging stage controls focus on material integrity. Ultrasonic testing uses high-frequency sound waves to detect internal voids, inclusions, or cracks, and suits thick components such as forged blocks and flanges. Magnetic particle inspection detects surface and near-surface cracks in ferromagnetic materials. Dye penetrant testing identifies hairline cracks, porosity, or laps on smooth surfaces. Radiographic testing uses X-rays or gamma rays for internal flaws in high-integrity components. Microstructure analysis and macroscopic examination of sample cuts catch cracks, folds, laps, underfilling, inclusions, segregation, and shrinkage cavities early.
Process control matters as much as inspection. Precise temperature control is critical during drop forging. Automated heating systems with real-time temperature monitoring maintain optimal forging conditions and minimize overheating or underheating, which can cause cracks, warping, or other defects. Automation also reduces human error and ensures batch-to-batch repeatability. In-process monitoring covers forging temperature, deformation ratio, process consistency, and component forming quality. Inspection adds CMM dimensional measurement, ultrasonic testing, magnetic particle testing, hardness testing, mechanical testing such as tensile checks, and metallographic analysis.
Machining stage controls verify tolerances against the drawing. The table below summarizes the main techniques.
Inspection Technique Nature Key Capability / Accuracy Typical Use Coordinate Measuring Machines (CMM) Contact (touch probe) or optical sensors Accuracy typically ±0.0001″ to ±0.0005″; CAD comparison and GD&T evaluation Gold standard for precision dimensional inspection Optical Measurement Systems Non-contact vision/laser Rapid inspection of profiles, edges, freeform surfaces; colorized deviation maps Delicate features or complex geometries where probing is difficult Optical Comparators Non-contact silhouette projection Magnified profile comparison against overlay drawings Rapid 2D profile verification in high-volume shop-floor settings Hand Tools & Indicators Contact, manual Routine dimensional checks; digital output for SPC tracking In-process verification and shop-floor monitoring Surface Roughness Instruments Contact stylus or non-contact Quantify Ra, Rz, Rmax surface texture parameters Verifying surface finish requirements In-process inspection monitors critical dimensions and features during machining, after each setup or at intervals. Problems are caught immediately and process adjustments are made before scrap accumulates. Statistical process control tracks measurement data on control charts over time. Trends toward specification limits become visible, which enables proactive correction and distinguishes normal variation from special causes. First article inspection thoroughly verifies the first part and validates the process before full-rate production.
Measurement environment affects results. Temperature-controlled measurement rooms maintain consistent conditions to prevent thermal expansion from corrupting measurements. For the highest-precision work, CMMs operate in environments held to ±1°F stability. The thermal expansion coefficient of typical steel means a 1°F change alters length by roughly 0.00000633″ per inch. Inspection at the tightest tier, roughly ±0.0002–0.0005 in (±0.005–0.013 mm), requires a CMM in a temperature-controlled environment, air gauging resolving to 0.1 µm, or electronic bore gauges. Hand-held instruments cannot reliably discriminate at these bands. Tolerance specification forms a three-way contract between design intent, the process that holds the band, and the inspection method that verifies it. A tolerance no available method can verify becomes a drawing liability.
An integrated workflow adds cross-stage checkpoints that separate vendors cannot replicate.
- Early near-net-shape alignment. Verify incoming blank consistency before machining. High blank variation turns marginal parts into scrap once machining exposes deviation, so cross-stage visibility is needed to catch variation before added cost.
- In-process machining control. Treat precision machining as a controlled stage. Hold tight tolerances, functional interfaces, and sealing surface conditions, with dimensional inspection performed continuously throughout the process.
- Post-machining verification and traceability. After geometry is complete, confirm performance conditioning, surface treatment, and verification. Many failures occur in these stages if treated as supplementary rather than integral.
- Heat treatment compliance. Control performance conditioning to achieve specified hardness at surface or core, verified against standards such as CQI-9.
- Final validation against industry requirements. Confirm compliance with applicable standards including ISO 9001, AS9100, ITAR, material traceability, and first article inspection.
The checkpoint controls deserve detail. In-process machining control covers heat- and wear-controlled cutting for titanium, nickel, and high-strength aluminum. Workholding and tool-health monitoring prevent chatter and wall distortion. Rough–relieve–finish sequencing maintains stress stability. Post-machining inspection and traceability rely on CMM and optical metrology proof of tolerances, serialized traceability of batch, process revision, and heat-lot data, and certified controlled finishing or coating. First article inspection to AS9102 qualifies the process, not just a single part, against all design requirements before full production release. Configuration management tracks serialized parts, material heats, process revisions, and drawing changes across the lifecycle for field-issue traceback. Risk and safety controls embed risk assessment, nonconformance control, and product safety analysis as design inputs. Supply chain integration governs who machines parts and how work is documented through approved supplier lists, regular audits, and counterfeit-prevention rules.
The documentation package closes the loop. It includes in-process inspection records showing measurements taken during machining, final inspection records with dimensional results against drawing callouts, material certifications with heat number and mill test report traceability, a complete AS9102 First Article Inspection Report for first articles, and demonstrated process capability data such as Cpk for key characteristics. This record set supports OEM manufacturing programs that require full traceability from billet to finished part.
The integrated approach serves automotive, construction machinery, marine, rail, and industrial power plant applications. Buyers in these sectors can send drawings or technical requirements for review and receive a process recommendation that matches load requirements, tolerance needs, and production volume.
The forging process and precision machining form one integrated workflow. Forging establishes strength and material integrity. Machining establishes accuracy and function. The right combination depends on load requirements, tolerance needs, and production volume. The two processes are partners, not competitors. This approach serves automotive, construction machinery, marine, rail, and industrial power plant applications. Our in-house precision forging and CNC machining deliver 18Xh3a alloy steel components ground to GB 6 / ISO 6 / AGMA 10, with surface hardness of HRC 58–62, as a single-source solution for custom mechanical parts. Share your drawings or technical requirements for review.
FAQ
Do forged metal components always require precision machining?
Not always. Simple, non-critical forgings may ship as-forged. Most custom mechanical parts with bearing seats, threads, or mating faces need precision machining to meet drawing tolerances and surface finish requirements.
How much material does the forging process leave for machining?
The finish allowance depends on part size and shape. Vendor and buyer agree on the value. A finish-all-over specification oversizes every surface so precision machining can clean up all faces.
What information should buyers include when requesting a quote?
Buyers should share the component drawing, material grade, tolerance callouts, surface finish, hardness, inspection standard, and annual volume. These details let the supplier recommend the right forging process and OEM manufacturing route.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.